Most small print shops lose money on transfers before the press even warms up. The culprit is rarely ink or powder. It is empty film. A customer orders six shirts with six different logos, and each logo gets its own run, its own roll advance, and its own slice of setup time. Multiply that across a week of small orders and the waste becomes a line item you can feel on your margins. A DTF Gangsheet solves that problem by treating many small jobs as one printed surface, and once you understand how to build one well, the savings compound.
What a DTF Gangsheet Actually Is
Direct-to-film printing works by printing a design in reverse onto a PET film, dusting it with adhesive powder, and curing the powder into a flexible layer. You then press the film onto fabric, peel it cold, and the design sits on top of the garment like a soft, stretchy sticker.
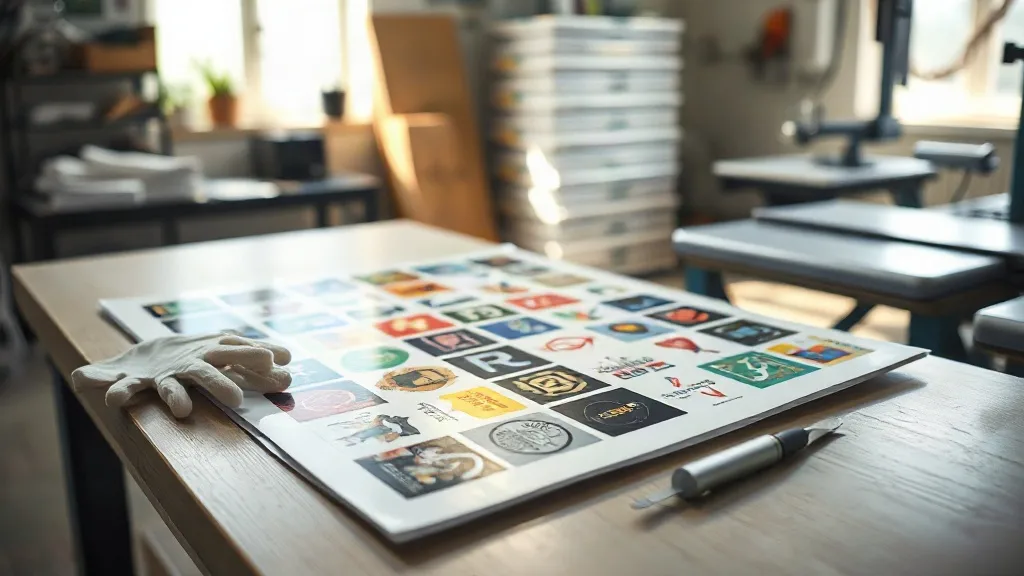
A gangsheet is simply a large piece of that film with multiple designs arranged on it. Instead of feeding a 12-inch strip for a 3-inch logo, you fill a 22-by-60-inch panel with everything queued for the day: names, numbers, sponsor logos, pocket prints, and a handful of one-off art pieces. The printer makes one pass. The cutter separates the pieces. The operator stacks them by order.
The reason this matters financially is that DTF costs scale with film area and printer time, not with the number of designs. Two designs on one sheet cost nearly the same to print as one design on the same sheet. That single fact is the entire economic argument for batching.
Why Shops That Batch Outperform Shops That Don't
Walk through a busy transfer shop on a Friday and you can usually tell within five minutes whether they gang their work. The tell is not the equipment. It is whether the printer is running continuously or stopping every few minutes for a new file.
Film utilization
A single small design printed alone might use 15 percent of the film that passes through the machine. The other 85 percent is blank PET that you paid for, powdered, cured, and threw away. Gang sheets push utilization into the 70 to 90 percent range with decent nesting. On a shop running a few hundred transfers a week, that difference is not a rounding error.
Printer throughput
Every job start and stop costs time: purging, alignment checks, and the operator walking back to the computer. Gang sheets turn twenty small jobs into one long run. The printer stays in its rhythm, white ink layers stay consistent, and the operator spends the saved time on trimming and packing instead of babysitting the feed.
Powder and cure efficiency
Powder application is easier to control on a larger continuous sheet than on scattered small pieces. Adhesive coverage is more even, and the shaker has fewer opportunities to over-apply on edges. Cured sheets also stack and store more neatly than loose small transfers, which matters more than most people admit once order volume climbs.
How to Lay Out a Sheet That Prints Clean
Layout is where gang sheets succeed or fail. A crowded sheet with no breathing room will print fine and then fall apart at the press.
Leave real spacing between designs
Give each design at least 0.25 inch of clearance, and closer to 0.5 inch if any of them have heavy ink coverage. Transfers need room for trimming, and the powder layer needs a clean margin so it does not bridge two designs into one unusable blob.
Group by color load
Place designs with heavy white underbases near each other rather than scattering them across the sheet. The white layer is the thickest and slowest part of the print, and grouping high-coverage art keeps the printhead's workload steadier. It also makes it easier to spot a white ink dropout before the sheet is cured.
Nest irregular shapes
Logos with wide empty areas can often interlock. Rotate a long banner design 90 degrees and slot smaller pieces into the gaps. Most RIP software includes an auto-nesting feature, but check its output by eye. Auto-nesting optimizes for area, not for trim-ability, and it will occasionally wedge two designs so close that your cutter operator has nothing to grab.
Respect the gripper and cut zones
Every printer and cutter has margins it cannot use. Keep designs a safe distance from the leading edge and from the sides. A design printed into the gripper zone is a design you will reprint.
Common Mistakes That Waste a Whole Sheet
- Mixing garment types on one sheet without noting it. A transfer sized for a cotton tee may not press cleanly on a nylon jacket. If you batch across fabric types, label each piece clearly.
- Forgetting the mirror. Film prints in reverse. A gang sheet built from unmirrored files produces a sheet of unreadable text, and there is no fixing it after cure.
- Ignoring color consistency across the sheet. If two versions of the same logo appear on one sheet, make sure they are the same file. Slight color shifts between duplicates look like a printing defect to the customer.
- Overfilling to chase utilization. A sheet packed to 98 percent is usually a sheet with trimming problems. Aim for comfortable density, not maximum density.
- Skipping the test press. Always press one transfer from a new sheet configuration before running the full order. A five-minute check saves an hour of reprints.
Pricing and Turnaround: What Changes When You Gang
The customer-facing benefit of ganging is straightforward. You can quote a per-piece price that beats single-run pricing because your film and machine time per design drop sharply. Many shops pass part of that saving along to win volume orders and keep the rest as margin.
Turnaround improves too, but not automatically. Batching means waiting for the sheet to fill, so the shop has to decide how long to hold a queue. A practical approach is to set a daily cut-off: everything ordered before noon goes on tomorrow's sheet, and anything that arrives after waits for the next batch. Customers accept this readily when you explain it as a scheduled production cycle rather than a delay.
Storing and Handling Finished Sheets
Cured transfers are more durable than most people expect, but they are not indestructible. Store sheets flat or rolled loosely with the powder side protected. Keep them away from heat and direct sun, and avoid stacking heavy objects on top, which can crack the adhesive layer on thick white underbases.
When you cut a sheet into individual transfers, bag them by order immediately. Loose transfers from a large batch are the single most common source of shipping errors in transfer shops, and a labeled bag costs almost nothing.
Frequently Asked Questions
How many designs can fit on one DTF gangsheet?
It depends entirely on size and nesting. A sheet filled with small left-chest logos can hold dozens of pieces, while a sheet with full-back prints might hold only four or five. Build the layout around your actual order mix rather than a fixed target count.
Does ganging transfers reduce print quality?
No, provided spacing and margins are respected. Each design receives the same ink and powder treatment it would get alone. Quality problems on gang sheets almost always trace back to crowding, poor trimming margins, or a skipped test press.
Can I mix different fabric types on the same sheet?
You can print them together, but you should track which transfer is destined for which garment. Press settings vary by fabric, and a transfer intended for cotton may need different temperature or pressure on a synthetic blend. Label pieces clearly when batching across materials.
What file format works best for gang sheet layouts?
Vector files such as PDF, EPS, or SVG give the cleanest edges and scale without loss, which matters when you are arranging many pieces at different sizes. High-resolution PNG files work as well if they are built at final print size with transparency intact.
How long can a finished gangsheet sit before use?
Cured transfers store well for months when kept flat, dry, and out of direct heat. The adhesive layer is the part most sensitive to storage conditions, so avoid humid areas and never stack heavy items on top of a sheet you plan to press later.